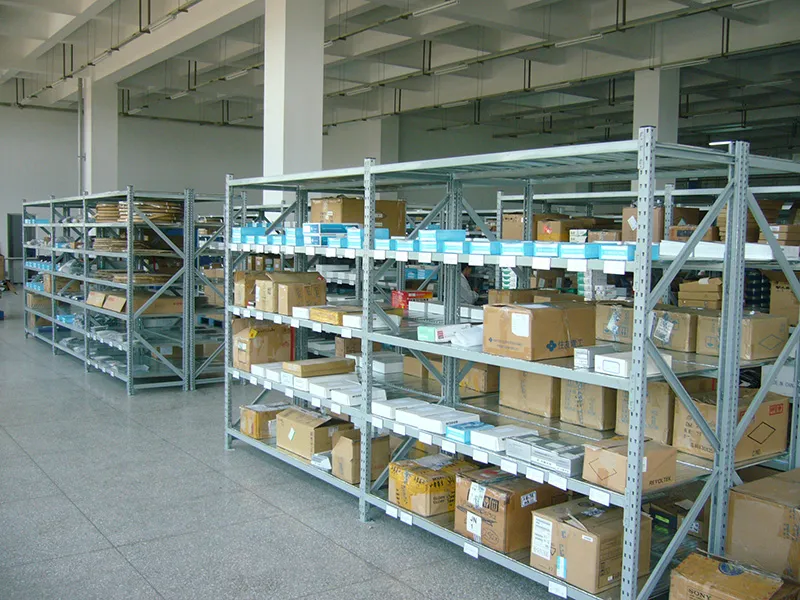
A well-known pharmaceutical manufacturing enterprise is constructing a new warehouse and plans to introduce shelves to improve warehouse space utilization and inbound/outbound efficiency. The warehouse is mainly used for storing finished pharmaceuticals and packaging materials. The core needs are to maximize the use of warehouse space, solve the problems of messy goods, low access efficiency and space waste under the traditional storage mode, and improve the accuracy of inbound and outbound operations to meet the increasing warehousing turnover needs after the enterprise’s production capacity is improved.
Showing Slide 1 of 3
Customized Solution
After in-depth communication and investigation with the customer, combined with the characteristics of pharmaceutical products that require classified storage by zones, as well as the customer’s warehouse space size and inbound/outbound operation process, we customized two sizes of long-span steel storage shelving according to the user’s product characteristics, taking into account safety, practicality and convenience:
2000×800×2000mm, single-layer load-bearing 300kg, 30 sets in total.
1500×800×2000mm, single-layer load-bearing 300kg, 26 sets in total.
Customer Benefits
Higher space utilization
Storage capacity increased by over 80% vs. traditional stacking via vertical space optimization.
Faster inbound/outbound
Zoned classified storage and clear labeling cut picking time by 60%, reduced errors and labor costs.
Easier management
Regular structure supports efficient inventory checks, integrates with existing systems for real-time monitoring, raised inventory turnover by 50% and freed up working capital.
Long-term practicality
Corrosion-resistant, durable steel shelving allows flexible layout adjustment or expansion, matching long-term business growth with high cost performance.
Scroll to Top
Get A Free Quote Now !
If you have any questions, please do not hesitate to contact us.